The coils are loaded onto the drum with precise centering, facilitated by servo motorized lateral side guides. When the operator inputs the sheet width on the control panel, these side guides expand laterally from the drum’s center to match the specified width. This ensures the coil is aligned correctly, preventing off-center positioning. As a result, the coil loading process becomes faster and safer.
Servo Motor Driven Decoiler
With the servo motor driven decoiling system, the coil loaded on the drum is uncoiled synchronously with the straightenerfeeder, preventing the high-strength coils from falling apart. With synchronously opened coil, an external load on the decoiler is prevented while the straightening group pulls the sheet.
Coil Loading Car
The coil can be safely loaded onto the coil loading car using a crane or forklift. The car’s Z-axis is driven by a hydraulic cylinder, while the Y-axis is powered by an A/C motor. To prevent the coil from tilting during loading, the car is equipped with safety pillars.
Introduction System
Hydraulically driven introduction system to introduce the coil into the straightener-feeder group without touching, quickly and reliably. This system with two hydraulically driven lower and upper shovels, can be adjusted according to the diameter of the loaded coil, with the telescopic extention nail on the lower shovel, it approaches the coil and takes the sheet metal onto the shovel. The sheet taken on the shovel fed to the straightening rollers contactless.
Crocodile Opening System
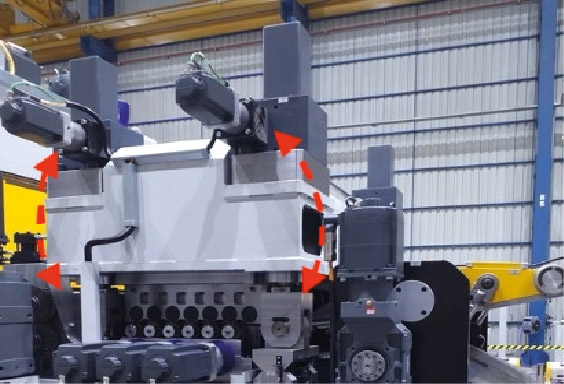
Straightener feeder group opened from the inlet side with approximate 20 degree angle. By the way it helps to introduce the sheet easily to the straightener group. This feature decrease the loss of time during the new coil loading. Opening of the group driven by hydraulic cylinders.
Servo Motor Driven Straightener Rolls
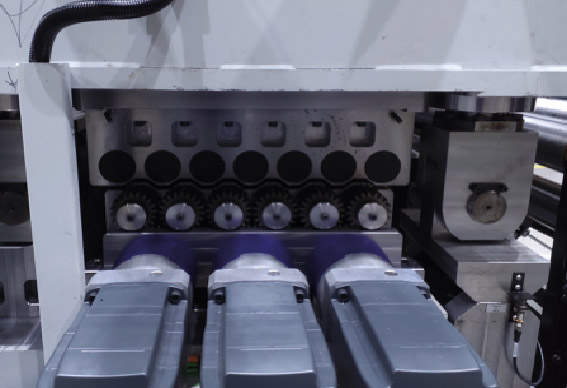
Straightening rolls are driven by three independent servo motors. With this way, the drive force transmitted to the straightening group is evenly distributed and the straightening rolls can drive the sheet synchronously. 2 servo motors for bottom rolls.
Support Rolled Straightener and Feeder Group
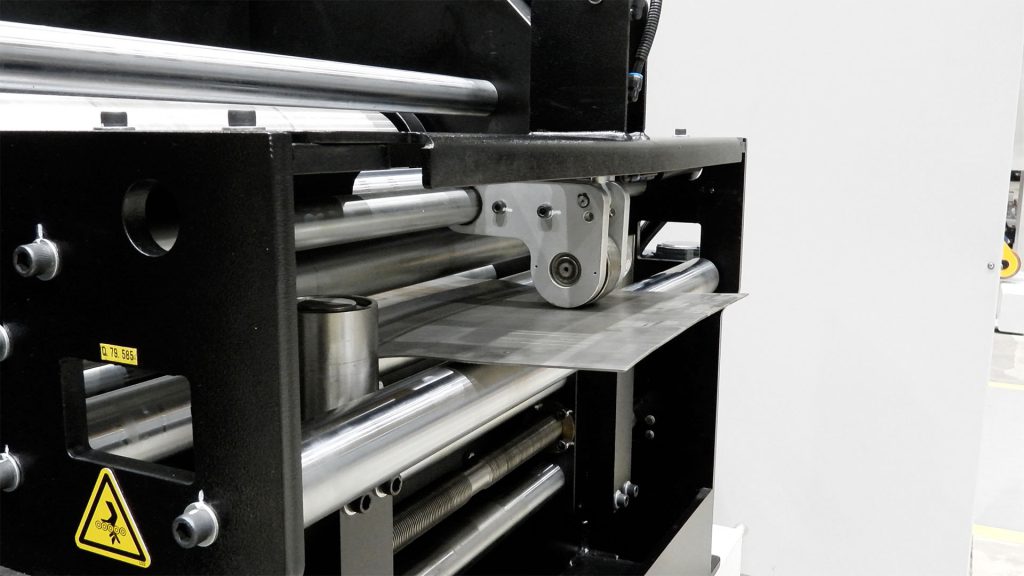
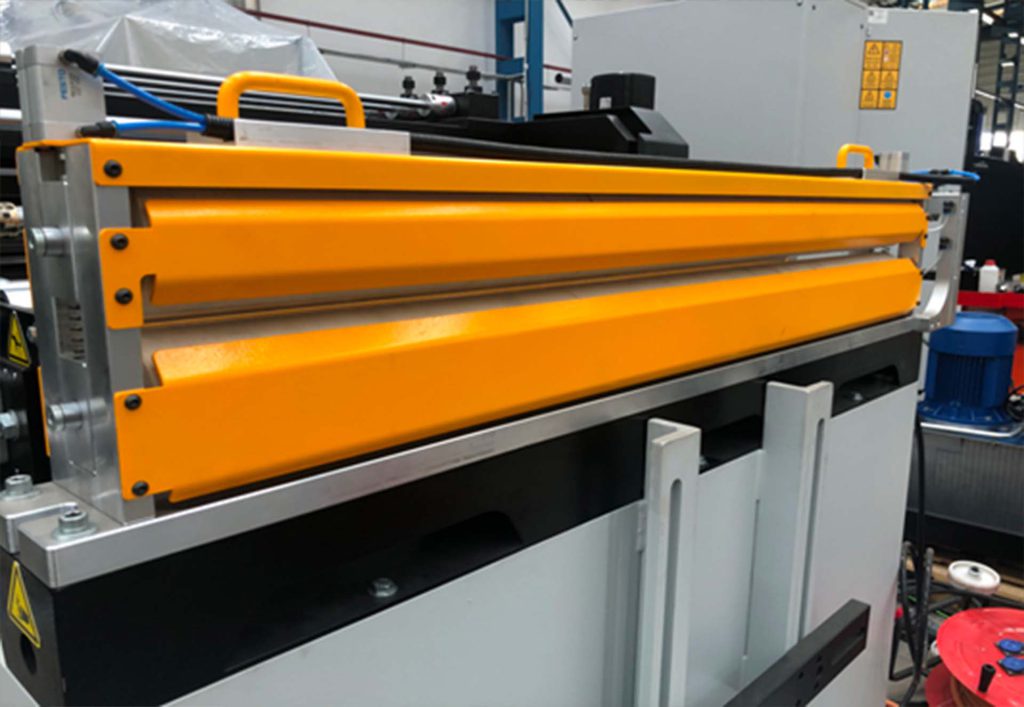
Rollers on straightener and feeder groups are supported from bottom and top with support rolls. By the way, rolls bending decrease to minimum level. Decreasing of the rolls bending provides high straightening quality.
Servo Motorized Straightener Adjustment
Straightener top rolls group adjustment has been done by servo motors automatically. First adjustment for each reference memorized to receipt system. Settings automatically adjusted when this reference recalled from receipt. To adjust the straightener group by servo motors gives more precision and high forces with prevents time lose of settings time.
G2 Die Recognizing System - Servo Motorized Side Guides
The guides at the inlet and outlet side of the straightener feeder group adjusted by servo motors. When the operator inputs the sheet width to the panel, these guides moves laterally from the center and goes to reference point. By the way sheet driven to the die from the center of the line. This setting is very fast and accurate with the help of servo motors. Die recognizing system can be included with the package.
G2 Die Recognizing System - Motorized Height Adjustment
Height adjustment of straightener feeder group automatically driven by a motorized system. When die height entered to the operator panel, machine rise or descend automatically according to entered value. Position control done by lineer ruler on the body
Allen Bradley control system - External Encoder Control
With the external encoder, feeded sheet length controled another time. Feeding rolls measurement and encoder wheel measurement controlled instantly during the feeding operation. Possible slipping of the sheet durning the feeding operation tolerated instantly.
Feeder Guideway - Optional
Between the feeding rollers and press bolster, there is a guideway that functions as bridge in order to moving sheet without bending.This guideway connected on the straightenerfeeder body, it acts in same way as the height setting changes.
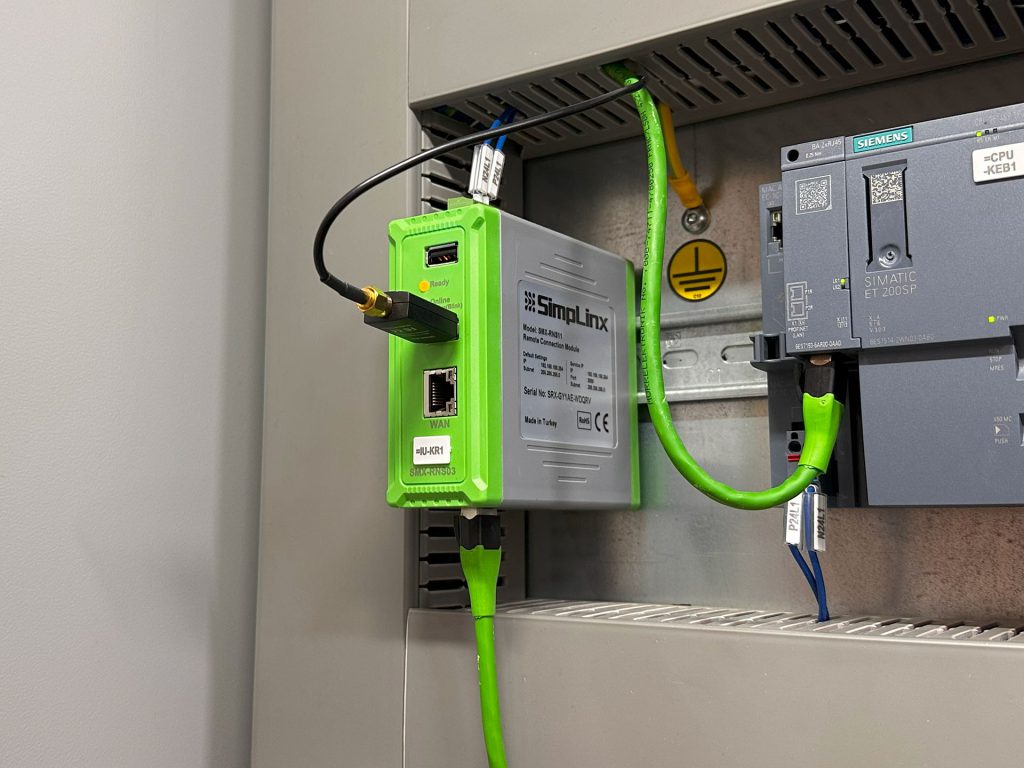
SimpLinx Remote Connection
Our machines are always accessible with the SimpLinx remote connection module. Intervention and diagnosis can be done by connecting to your machine remotely. Processes in the fastest way possible by our technical service team in case of any malfunction. It helps to connect without getting stuck cause of your port or firewall restriction procedures.
Sheet Positioning Inside Die with Hand Wheel
In progressive tools, from the introduction of the sheet into the die, the press is used in single stroke mode and the feeding system in manual mode until the first part falls. The advance of the sheet to the next operation after each stroke is done by the hand wheel with much more precisely and quickly. Thus, both the start time of mass production will be shortened and safer work will be provided in terms of safety.
Hydraulic Guillotine
Cutting Type
Hydraulic
Cutting Capacity
7,0mm @600mpa
Blade Gap Adjustment
No
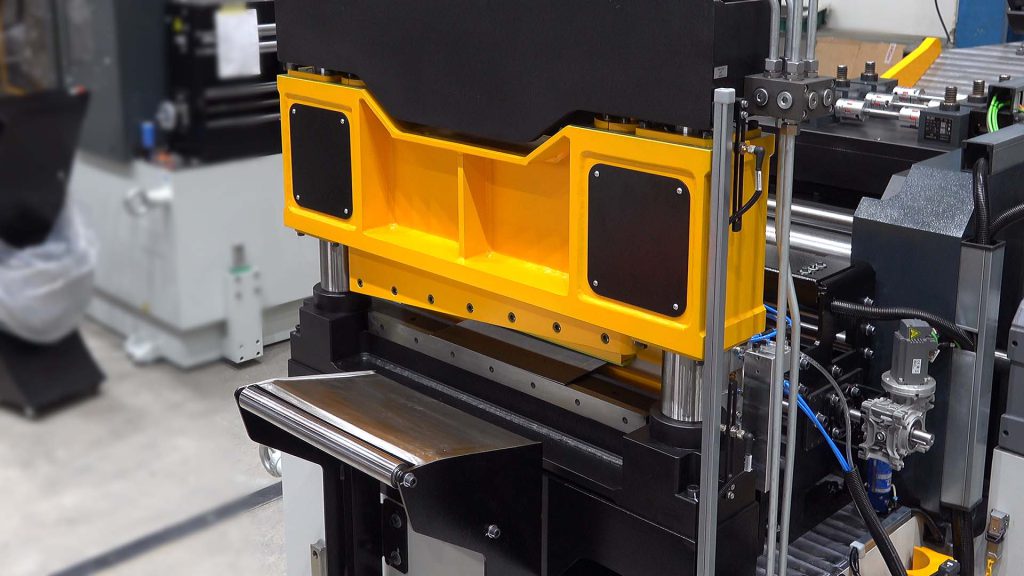
Guillotine Shear; cutting shear cuts sheet metal between feeder and die in case of operation stop for any reason.